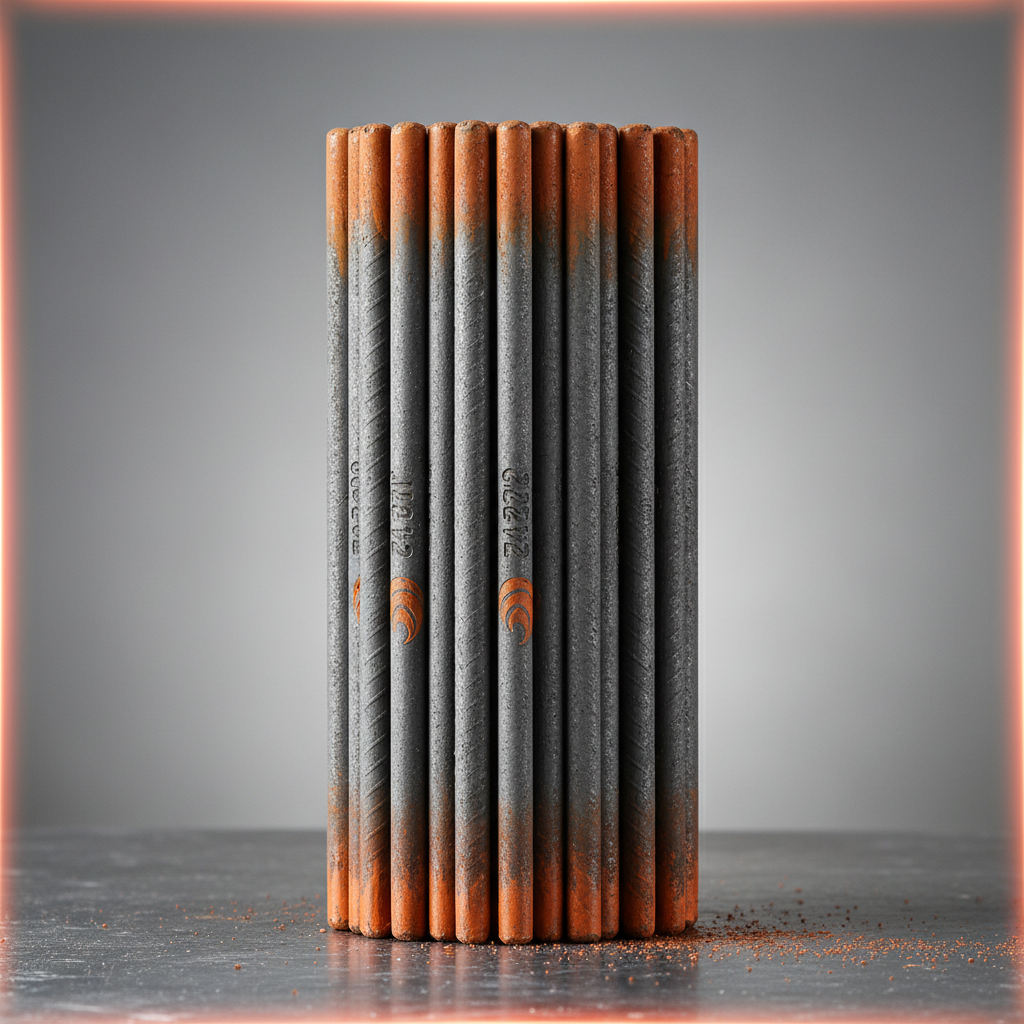
In the demanding world of high-precision metal fabrication, selecting the right filler material is critical for structural integrity. The concept of a specialized welding rod j421 represents the industry's constant drive toward materials that can bridge the gap between disparate metal types, ensuring that welds remain crack-free under extreme stress.
Across global manufacturing hubs, the challenge of joining high carbon steel and tool steel has historically led to brittle joints and premature failure. By implementing advanced duplex stainless steel technology, operators can now achieve high-strength bonds that maintain ductility, effectively solving the problem of hydrogen-induced cracking in complex industrial assemblies.
Understanding the technical specifications of a welding rod j421 allows engineers to optimize their welding parameters for both AC and DC currents. This flexibility, combined with superior crack resistance, makes it an essential tool for those operating in the cutting-tool and heavy machinery sectors.
Material Composition and Technical Properties of welding rod j421
The technical foundation of the welding rod j421—specifically based on the E312-16 duplex stainless steel specification—is its titanium-calcium coating. This unique chemical composition ensures that the welding process remains stable across various electrical configurations, allowing for seamless transitions between AC and DC power sources.
One of the most critical attributes of this material is its ferrite content, which sits at approximately 40%. This high ferrite level is the primary reason for the electrode's exceptional resistance to cracking, making it an ideal choice for high-stress environments where thermal expansion and contraction are frequent.
Application Scope for High Carbon and Tool Steels
The primary utility of the welding rod j421 lies in its ability to handle challenging materials such as high carbon steel and tool steel. These materials are notoriously difficult to weld due to their tendency to harden and crack during the cooling phase, requiring a filler material that can absorb stress.
Beyond single-material joints, this electrode is highly effective for welding dissimilar metals. In complex machinery, where a tool steel component must be joined to a different alloy, the duplex nature of the weld metal creates a compatible buffer zone that prevents metallurgical incompatibility.
Industries ranging from automotive mold making to heavy industrial tool manufacturing rely on these properties to ensure that their components can withstand high mechanical loads without suffering from joint failure or fatigue cracks.
Essential Pre-Welding Preparation and Baking Protocols
To achieve the maximum performance of the welding rod j421, strict adherence to preparation protocols is mandatory. The electrode must be baked at temperatures between 300-350℃ for one hour prior to use, ensuring that any residual moisture is eliminated from the coating.
Surface cleanliness is equally paramount. Before initiating the arc with a welding rod j421, the base metal must be thoroughly cleaned to remove rust, grease, moisture, and other impurities that could introduce contaminants into the weld pool.
For specialized cases involving hardenable steel or thick, complex workpieces, preheating is necessary. When using small currents, the workpieces should be preheated to 150℃ to reduce the cooling rate and further mitigate the risk of cold cracking in the heat-affected zone.
Performance Analysis and Welding Position Efficiency
The operational versatility of the welding rod j421 is demonstrated by its ability to be used in all standard welding positions. Whether the task is PA (flat), PB (horizontal), PC (vertical up), PD (overhead), PE, or PF, the electrode maintains a stable arc and excellent slag detachability.
This multi-position capability reduces the need for expensive workpiece rotation equipment, allowing technicians to perform high-quality repairs in situ, even in restricted industrial spaces or remote field locations.
Welding Performance Metrics for welding rod j421
Material Requirements and Compliance Standards
The integration of the welding rod j421 into a production line must follow strict material substitution and inspection systems. All raw materials, including the steel plates and the electrodes themselves, must be verified against technical drawings and possess certificates of conformity.
To ensure mechanical integrity, the principle of equal strength between the weld metal and the base metal is applied. The welding rod j421 is designed to meet rigorous standards such as GB/T 5117, GB/T 5118, and GB/T 8110, ensuring the weld is never the weakest point of the assembly.
Logistics, Packaging, and Storage Management
Efficient supply chain management for the welding rod j421 begins with standardized packaging to prevent moisture ingress. The electrodes are packed in 5kg boxes, with 4 boxes per carton (20kg total), and 50 cartons per pallet to ensure stability during international transit.
For large-scale industrial procurement, the shipping capacity is optimized for 21MT to 26MT per 1X20" FCL, allowing for cost-effective bulk transport to global manufacturing sites. This structured packaging ensures that the delicate titanium-calcium coating remains intact from the factory to the workshop.
Storage is the final critical link; after baking, the welding rod j421 must be kept in an incubator and only removed as needed. It is strictly advised that the rods should not be baked more than twice to avoid degrading the coating's chemical properties.
Comparative Quality Metrics for Industrial Welding
When evaluating the welding rod j421 against standard electrodes, the primary differentiator is its crack resistance in high-carbon environments. While standard rods may suffer from cold cracking, the duplex structure provides a safety margin that is indispensable for tool steel applications.
The balance of mechanical properties ensures that the weld metal's strength is not lower than that of the base metal, a requirement that is rigorously tested under GB/T standards. This ensures that the welded joint can handle the same operational loads as the rest of the component.
Ultimately, the value of the welding rod j421 is found in its reliability. By minimizing the risk of failure in critical joints, companies can reduce warranty claims, lower maintenance costs, and increase the overall lifespan of their industrial tools.
Comparison of welding rod j421 Performance across Steel Grades
| Base Material |
Crack Resistance |
Weld Strength |
Ease of Use |
| High Carbon Steel |
Excellent (9/10) |
High (8/10) |
Moderate (7/10) |
| Tool Steel |
Superior (10/10) |
High (9/10) |
Moderate (7/10) |
| Dissimilar Metals |
Very Good (8/10) |
Moderate (7/10) |
High (9/10) |
| Alloy Steel |
Good (7/10) |
High (8/10) |
High (9/10) |
| Hardened Steel |
Excellent (9/10) |
Moderate (6/10) |
Low (5/10) |
| Mild Steel |
Excellent (10/10) |
Very High (10/10) |
Very High (10/10) |
FAQS
The welding rod j421 is primarily used for welding high carbon steel, tool steel, and dissimilar metals. Its duplex stainless steel composition and high ferrite content (about 40%) make it exceptionally resistant to cracking, which is the most common failure point when welding hardenable steels.
Yes, to ensure optimal performance and prevent porosity, the electrode must be baked at 300-350℃ for 1 hour before use. It should be stored in an incubator after baking and should not be baked more than twice to avoid damaging the titanium-calcium coating.
Absolutely. One of the key advantages of the E312-16 based welding rod j421 is its excellent process performance, which allows it to be used effectively with both alternating current (AC) and direct current (DC) power sources.
For welding hardenable steel, especially when using small currents on complex or thick workpieces, the base metal should be preheated to 150℃. This reduces the thermal shock and further minimizes the risk of cracking in the weld joint.
The electrode is highly versatile and can be used in all standard positions, including PA (flat), PB (horizontal), PC (vertical up), PD (overhead), PE, and PF, making it suitable for a wide range of structural and repair tasks.
It is packaged in 5kg boxes, with 4 boxes per carton (20kg), and 50 cartons per pallet. For shipping, it can be loaded at 21MT to 26MT per 1X20" FCL, ensuring secure transport and protection of the electrode coatings.
Conclusion
The welding rod j421 serves as a critical solution for the complex challenges associated with welding high carbon and tool steels. By combining a duplex stainless steel core with a titanium-calcium coating and maintaining a high ferrite content, it provides an unparalleled balance of crack resistance, strength, and versatility across all welding positions.
For manufacturers looking to enhance the reliability of their tool assemblies, investing in high-quality electrodes and strictly following pre-welding baking and cleaning protocols is the most effective path toward zero-defect production. We invite you to explore our full range of professional welding solutions to optimize your industrial output. Visit our website: www.steeltoolschina.com