In the specialized world of industrial metallurgy, selecting the correct filler material is the difference between a structural failure and a lifelong bond. For those working with cast iron, a material notorious for its brittleness and propensity to crack, the precision of the electrode is paramount. Whether you are repairing heavy machinery or fabricating custom components, understanding the role of a welding rod 3.2mm and high-nickel alloys is essential for achieving professional-grade results.
The global demand for high-performance welding consumables has surged as infrastructure projects move toward more durable, sustainable materials. In the context of cast iron repair, the industry has shifted toward pure nickel cores and strong reduction graphite-type coatings to mitigate the risks associated with thermal stress. This evolution ensures that critical engine blocks, pump housings, and industrial molds can be restored without the risk of catastrophic fracturing during the cooling process.
For professionals seeking the ideal balance between deposition rate and control, the welding rod 3.2mm remains a versatile standard in the workshop. By utilizing AWS ENi-CI Z308 specifications, operators can ensure a high-quality weld that is easy to machine and highly resistant to cracking, providing a reliable solution for complex cast iron challenges across the globe.
Technical Specifications of ENi-CI Z308
The AWS ENi-CI Z308 is engineered as a pure nickel welding core, specifically designed to address the inherent difficulties of welding cast iron. Its strong reduction of graphite-type coating ensures that the molten pool remains stable, significantly reducing the risk of carbon migration and subsequent brittle phase formation. When utilized as a welding rod 3.2mm, it provides a precise balance of heat input and filler deposition.
One of the most significant advantages of this specification is its exceptional crack resistance and post-weld processability. Because the nickel-based weld metal remains ductile, it can absorb the stresses generated as the surrounding cast iron contracts during cooling. This makes it the primary choice for repairing critical industrial components where structural integrity is non-negotiable.
Operational Flexibility in Modern Welding
Versatility in the workshop is a key driver of productivity. The ENi-CI Z308 electrode is designed for AC and DC dual-purpose use, allowing technicians to adapt to whatever power source is available on-site. This flexibility reduces downtime and ensures that high-quality repairs can be performed in both controlled shop environments and remote field locations.
Unlike many other cast iron fillers, this specific formulation is designed for cold welding applications. A major operational benefit is that it does not necessitate the preheating of the weldment. This eliminates the need for expensive heating blankets and prolonged wait times, streamlining the workflow for urgent machinery repairs.
The ease of operation associated with the welding rod 3.2mm size allows for better arc control and a smoother bead profile. This is particularly important when working on thin-walled cast sections where excessive heat could lead to burn-through or unwanted metallurgical changes.
Critical Pre-Welding and Handling Requirements
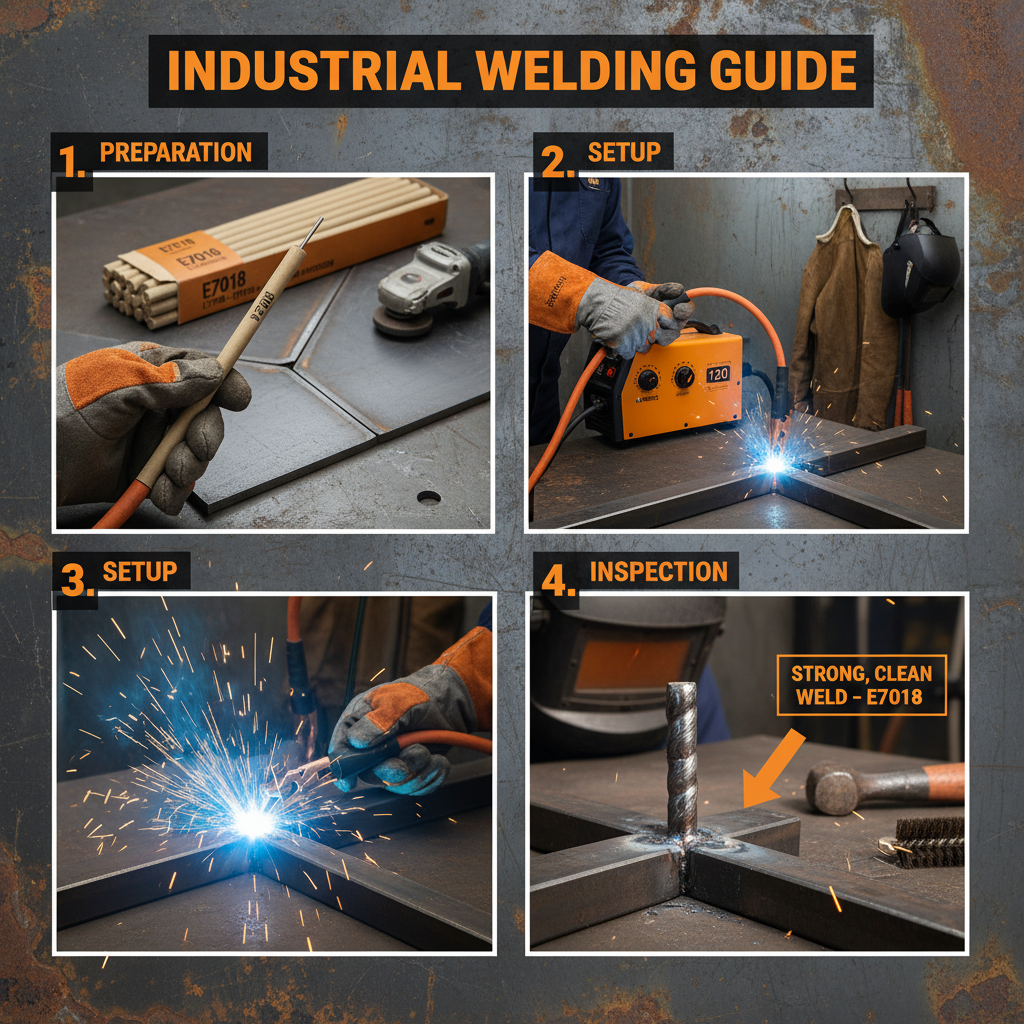
Preparation is the foundation of a successful weld. For the ENi-CI Z308, a strict baking regimen is required to ensure the coating is free of moisture. Electrodes must be baked for 1 hour at a temperature of 150±10℃ before use to prevent hydrogen-induced porosity and ensure arc stability when using a welding rod 3.2mm.
To further safeguard the weld, technicians should employ hammering techniques on the welding seam. This mechanical action helps eliminate welding stress and prevents the formation of micro-cracks during the solidification phase, which is a common failure point in cast iron joining.
Furthermore, the purity of the base metal penetration is critical. By utilizing a welding rod 3.2mm with small current settings, operators can narrow the white band width—the brittle zone created during welding—thereby improving the overall crack resistance and machining properties of the finished part.
Impact of Current Control on Weld Integrity
Precision in current selection is what separates a professional repair from a failed attempt. When utilizing the welding rod 3.2mm for cast iron, "small current welding" is the recommended approach. Lowering the amperage reduces the heat-affected zone (HAZ), which in turn limits the formation of hard, brittle martensite in the cast iron.
By maintaining a lower heat input, the welder can better control the penetration depth and minimize the risk of impurities from the base metal leaching into the weld pool. This technical discipline ensures that the final joint possesses the necessary ductility to withstand operational vibrations and thermal cycling.
Welding Performance Comparison for 3.2mm Electrodes
Strategic Welding Positions and Techniques
The application of ENi-CI Z308 is optimized for specific welding positions, namely PA (Flat) and PB (Horizontal-Vertical). Mastering these positions with a welding rod 3.2mm ensures that the weld pool is managed effectively, preventing sagging and ensuring a full-penetration bond.
Technical proficiency in these positions allows for better control over the bead shape and the ability to overlap passes without introducing excessive heat. This is crucial for building up surface wear or filling deep cracks in heavy cast iron components where gravity affects the molten nickel.
Managing Distortion and Thermal Stress
Distortion is an inevitable challenge in welding, but it can be managed through disciplined technique. When using a welding rod 3.2mm, the goal is to minimize the localized heat buildup. Rapid cooling or quenching is strictly prohibited for hardenable welded parts, as this almost guarantees the formation of brittle cracks.
The cooling process must be gradual. For components requiring annealing, rectification should be performed before the annealing process to eliminate internal stresses. Ensuring the part is placed steadily during this phase prevents the component from deforming under its own weight at high temperatures.
Mechanical correction, such as hammering or pressing, is strictly forbidden within the "blue brittle" temperature range of 300℃ to 500℃. Attempting to force a part back into alignment during this critical window can lead to immediate fracture, undoing all the precision work achieved with the welding rod 3.2mm.
Advanced Post-Weld Correction Standards
When deformation occurs, flame straightening is the professional's tool of choice. The heating temperature for flame correction should typically range between 700℃ and 850℃ (fuchsia color). It is imperative that the temperature does not exceed 900℃ (bright red) for low alloy structural steels to avoid damaging the metallographic structure.
A key rule of thumb is to avoid repeated heating of the same area. Continuous thermal cycling can alter the mechanical properties of the steel and the weld, potentially leading to softening or unintended hardening. This disciplined approach preserves the integrity established by the welding rod 3.2mm.
Consistency in tension and compression is also vital; do not perform repeated corrections of opposite forces on the same part. By following these strict thermal guidelines, technicians can restore the geometry of a part without compromising the metallurgical bond of the nickel weld.
Guidelines for Thermal and Mechanical Correction of Weldments
| Correction Method |
Temperature Range |
Risk Factor |
Recommended Action |
| Mechanical Hammering |
< 300℃ / > 500℃ |
Brittle Cracking |
Avoid 300-500℃ range |
| Flame Straightening |
700℃ - 850℃ |
Grain Growth |
Maintain "Fuchsia" heat |
| Overheating |
> 900℃ |
Structural Change |
Strictly Prohibited |
| Rapid Cooling |
Ambient/Water |
Thermal Shock |
Prohibit Watering |
| Annealing |
Process Specific |
Internal Stress |
Rectify before annealing |
| Cold Welding |
Ambient |
White Band Formation |
Use small current settings |
FAQS
Baking the ENi-CI Z308 electrode at 150±10℃ for one hour is critical to remove moisture from the coating. Moisture can lead to the introduction of hydrogen into the weld pool, which causes porosity and increases the likelihood of cold cracking in the cast iron base metal. Proper baking ensures a stable arc and a dense, high-quality weld bead.
Yes, the ENi-CI Z308 is specifically designed for cold welding applications. One of its primary advantages is that it does not require the base metal to be preheated. This makes it ideal for rapid repairs and for situations where heating the entire component is impractical or could cause unwanted distortion.
The blue brittle range occurs between 300℃ and 500℃. In this temperature window, the material becomes exceptionally susceptible to brittle fracture. Performing mechanical corrections, such as hammering or pressing, within this range can cause the weld or the base metal to crack instantly, even if the weld was performed correctly.
Small current welding refers to operating the machine at the lower end of the recommended amperage range for a welding rod 3.2mm. This minimizes heat input, which reduces the width of the "white band" (the brittle transition zone) and prevents the base metal from overheating, thereby improving the ductility and machining properties of the joint.
Absolutely. The AWS ENi-CI Z308 is engineered for dual-purpose use, meaning it functions efficiently on both Alternating Current (AC) and Direct Current (DC) welding machines. This ensures that technicians can achieve high-quality results regardless of their power source.
The cooling process must be slow and controlled. You must strictly avoid watering or rapid air-cooling (quenching), as this causes severe thermal stress and cracking. For the best results, allow the part to cool naturally in still air or bury it in dry sand/vermiculite to slow the temperature drop.
Conclusion
Achieving a successful weld on cast iron requires a synergy of high-quality materials and disciplined technical execution. By utilizing the ENi-CI Z308 welding rod 3.2mm, operators can leverage the ductility of pure nickel to overcome the brittleness of cast iron. From the essential pre-welding baking process to the careful avoidance of the blue brittle temperature range, every step in the workflow is designed to eliminate stress and prevent cracking.
As industrial demands evolve, the importance of precision consumables and adherence to metallurgical standards becomes even more critical. We recommend that all technicians prioritize current control and gradual cooling to maximize the lifespan of their repairs. For those seeking industry-leading welding solutions and high-performance electrodes, visit our website: www.steeltoolschina.com.